
Cart
0
your cart

No items found.
Product is not available in this quantity.

A road contractor may handle several types of projects in the same year. One month, the team may resurface municipal streets. The next, it may pave an industrial access road or repair a provincial highway. Each project has different production demands, traffic restrictions, haul distances, and completion deadlines. Therefore, choosing an asphalt mixing plant requires more than checking its rated capacity.
A 120 TPH mobile asphalt plant can be a practical investment for contractors who need substantial hot mix asphalt production and the flexibility to move between project locations. However, its suitability depends on actual paving demand, aggregate supply, asphalt mix requirements, transportation costs, and the time available for installation and relocation. This guide explains how to evaluate these factors before committing to a purchase.

Before comparing project types, contractors should understand the difference between rated capacity and actual production. A plant rated at 120 tons per hour can produce up to that amount under specified operating conditions. Actual output depends on aggregate moisture, mix temperature, material gradation, equipment configuration, and operating efficiency.
For preliminary planning, a contractor can estimate production using the following formula:
Daily Asphalt Production = Rated Capacity × Effective Production Hours Per Day
For example, a 120 TPH plant operating for six effective production hours could theoretically produce 720 tons per day. At eight effective hours, the figure would reach 960 tons. These estimates assume the plant sustains its rated output throughout the stated hours.
Real projects rarely operate under perfectly consistent conditions. Aggregate moisture, warm-up time, mix changes, truck availability, maintenance, and paving interruptions can reduce output. Contractors should therefore use realistic operating assumptions rather than treating rated capacity as a guaranteed daily result.
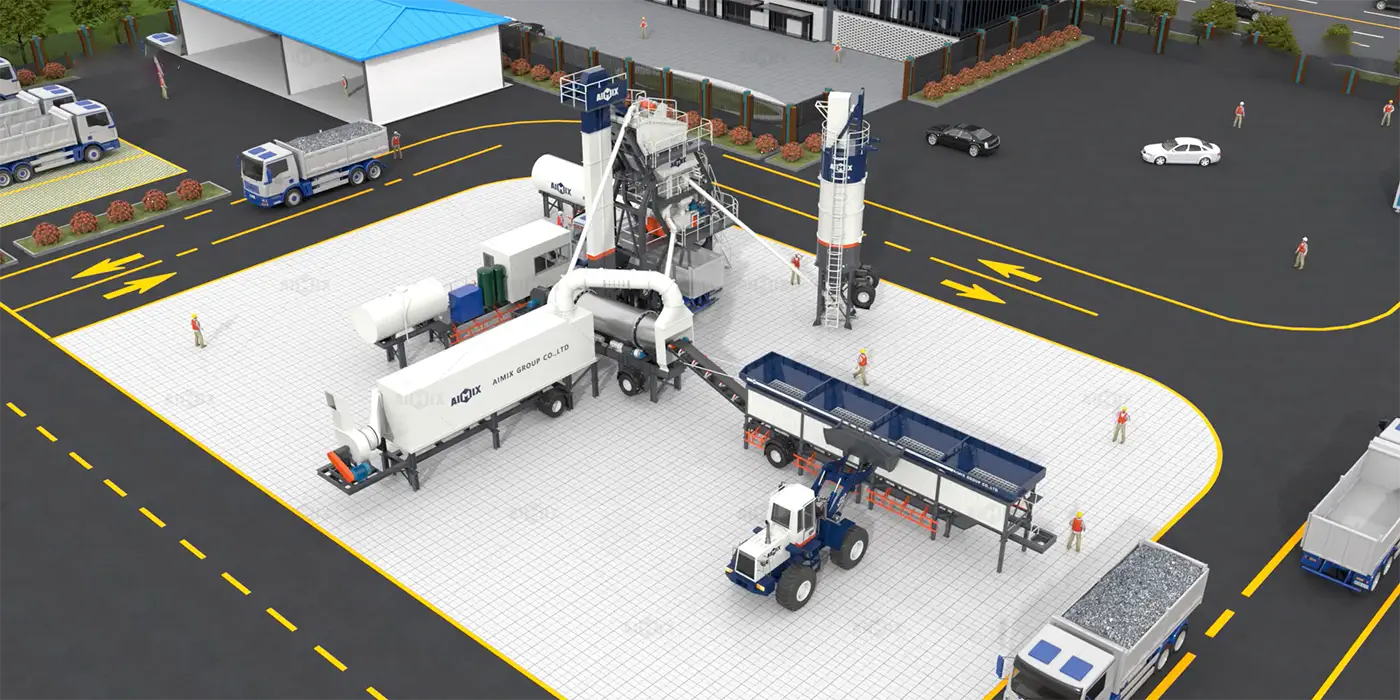
A mobile asphalt plant can help contractors serve projects in different locations without investing in a permanently fixed production site for every contract. Depending on the plant design, its modular components may simplify transportation, setup, and relocation.
However, mobile does not mean that every component can travel as one road-ready unit. Contractors must confirm transport dimensions, component weights, lifting requirements, assembly procedures, foundation or ground preparation needs, utility connections, and local transport permits.
With these practical limitations in mind, the next step is to assess whether the plant matches the production demands of each road category.
Municipal road contracts often involve urban streets, residential access roads, intersections, parking areas, and local road rehabilitation. These projects may require frequent changes in paving locations and careful coordination with traffic management teams.
A 120 TPH mobile asphalt plant can suit municipal contractors who manage multiple resurfacing projects or combine several small road sections into a larger paving schedule. It can also support contractors who supply asphalt to several nearby paving crews.
Not every municipal contractor needs 120 tons per hour. A small maintenance crew that only paves a limited area each week may struggle to keep the plant productive. The contractor could pay for unused capacity while still covering labor, fuel, maintenance, and site operating costs.
Urban sites also create practical challenges. Limited land, nearby residents, dust and noise controls, truck queues, and restrictions on operating hours can affect plant location and production schedules. A mobile plant still requires a suitable site and approval from the relevant authorities.
Therefore, municipal contractors should estimate the combined asphalt demand of their current and upcoming contracts. If several projects can share production efficiently, a 120 TPH plant becomes more attractive.

Industrial roads serve factories, warehouses, logistics parks, mining facilities, ports, and other heavy-duty operating areas. These projects may involve frequent truck movements, concentrated wheel loads, and construction schedules that must fit around ongoing industrial operations.
For industrial road contractors, production capacity matters because paving interruptions can disrupt material deliveries, equipment utilization, and site coordination. A 120 TPH mobile asphalt plant may provide a suitable production base for medium to large paving programs, depending on the required mix and daily tonnage.
Industrial roads do not all use the same asphalt mixture. The project specification may require particular aggregate gradations, binder grades, mix temperatures, or performance characteristics. The plant must support the required mix designs and quality-control procedures.
Contractors should also check the plant's configuration. The dryer, burner, screening system, hot aggregate bins, weighing equipment, mixer, dust collection system, and control system all affect production performance. A rated capacity alone cannot confirm that a plant will meet every project's technical requirements.
For industrial projects, the strongest case for a mobile plant usually comes from combining sufficient production capacity with reliable material supply and a practical site layout.
Provincial road projects can involve long road sections, multiple work fronts, remote locations, and varying access conditions. Some contracts require continuous paving over extended periods, while others divide construction into separate sections according to funding, weather, or traffic management requirements.
A 120 TPH mobile asphalt plant may support provincial road contractors who need to establish production near a project and move the plant when the work progresses to another location. This arrangement can reduce dependence on distant commercial asphalt suppliers when local production is technically and economically viable.
However, the actual benefit depends on the relationship between plant location and paving operations. A plant that moves too frequently may incur transportation, dismantling, assembly, commissioning, and downtime costs. Contractors should compare these expenses with the cost of hauling asphalt from an existing supplier.
Asphalt delivery is not simply a matter of moving the largest possible tonnage. Trucks must arrive within the project's delivery and temperature requirements, and the paving crew must maintain a coordinated workflow.
Consequently, a 120 TPH plant is most useful when its production rate matches the paving crew's consumption rate and the available truck fleet can sustain deliveries. If trucks cannot transport asphalt quickly enough, additional plant capacity may not improve daily paving output.
Daily output helps contractors determine whether a plant can support their contract schedule. Nevertheless, effective production hours matter more than the rated capacity alone. The following examples illustrate theoretical production under different operating schedules.
These figures are planning examples, not guaranteed production results. Actual output may be lower because of aggregate moisture, startup and shutdown time, mix changes, maintenance, material shortages, or interruptions in paving.
Contractors can estimate asphalt tonnage using the paved area, compacted layer thickness, and specified compacted mixture density.
Estimated Asphalt Tonnage = Paved Area × Compacted Thickness × Compacted Mix Density
Use consistent units in the calculation. For example, express area in square meters, thickness in meters, and density in tons per cubic meter to obtain the result in tons.
For a more reliable estimate, calculate each pavement layer separately and account for the actual project scope. The contractor should then compare total demand with the available paving days and effective daily production.
This approach helps answer a more useful question than rated capacity alone: can the plant supply the required asphalt volume within the contract period?
Purchasing a mobile asphalt plant involves more than the equipment price. Contractors need to evaluate the total investment against expected production, project duration, operating expenses, and future utilization.
A practical investment assessment should include the following costs:
Buying a plant may make sense when a contractor has sufficient recurring demand and can keep the equipment productive across multiple contracts. Outsourcing may be more practical when asphalt demand is irregular, project volumes are small, or suitable suppliers are readily available.
To compare the two options, calculate the delivered cost per ton under each scenario. Include material, production, transport, labor, maintenance, financing, and other relevant expenses. Avoid assuming that owning the plant automatically creates savings.
A contractor should also test different utilization scenarios. A delayed project, a short paving season, or a gap between contracts can change the investment result significantly.

Once the production and financial requirements are clear, contractors can evaluate the plant configuration and supplier support. A suitable plant must work under actual site conditions rather than only meet a capacity target on paper.
Before requesting a quotation, prepare the project information that determines the plant configuration. This helps the supplier provide a more relevant proposal and reduces the risk of comparing equipment with different specifications.
Clear answers allow contractors to compare suppliers based on total project suitability rather than purchase price alone.
A 120 TPH plant is not automatically the best choice for every contractor. The right capacity depends on the size and frequency of contracts, the paving rate, transport arrangements, and the expected workload over the equipment's service life.
Also compare fixed and mobile configurations. A stationary plant may suit a long-term production base with stable demand, while a mobile configuration may offer greater flexibility across project locations. Actual relocation time and cost depend on the specific equipment design.

A 120 TPH mobile asphalt plant can be suitable for contractors working on municipal, industrial, and provincial roads when their combined asphalt demand justifies the capacity. It can support multi-site operations, larger paving schedules, and projects where establishing production near the work offers a practical advantage.
However, the decision should rest on measurable project requirements. Estimate total tonnage, effective production hours, haul distance, truck availability, material conditions, installation costs, and expected annual utilization. Then compare the full cost of ownership with the cost of purchasing asphalt from external suppliers.
Planning a Road Construction Project? Contact AIMIX to discuss your expected asphalt output, project locations, mix requirements, and mobility needs. Share your estimated daily tonnage, working hours, and site conditions so our team can help you evaluate whether a 120 TPH mobile asphalt plant or another configuration better matches your construction plan.

